
Heavy Equipment Troubleshooting: A Global Field Guide to Fault Codes, Hydraulic Symptoms, and Parts Traceability
Step-by-step diagnostic frameworks for excavators, loaders, and dozers covering SAE J1939 codes, hydraulic symptom analysis, and genuine parts sourcing strategies for global fleets.
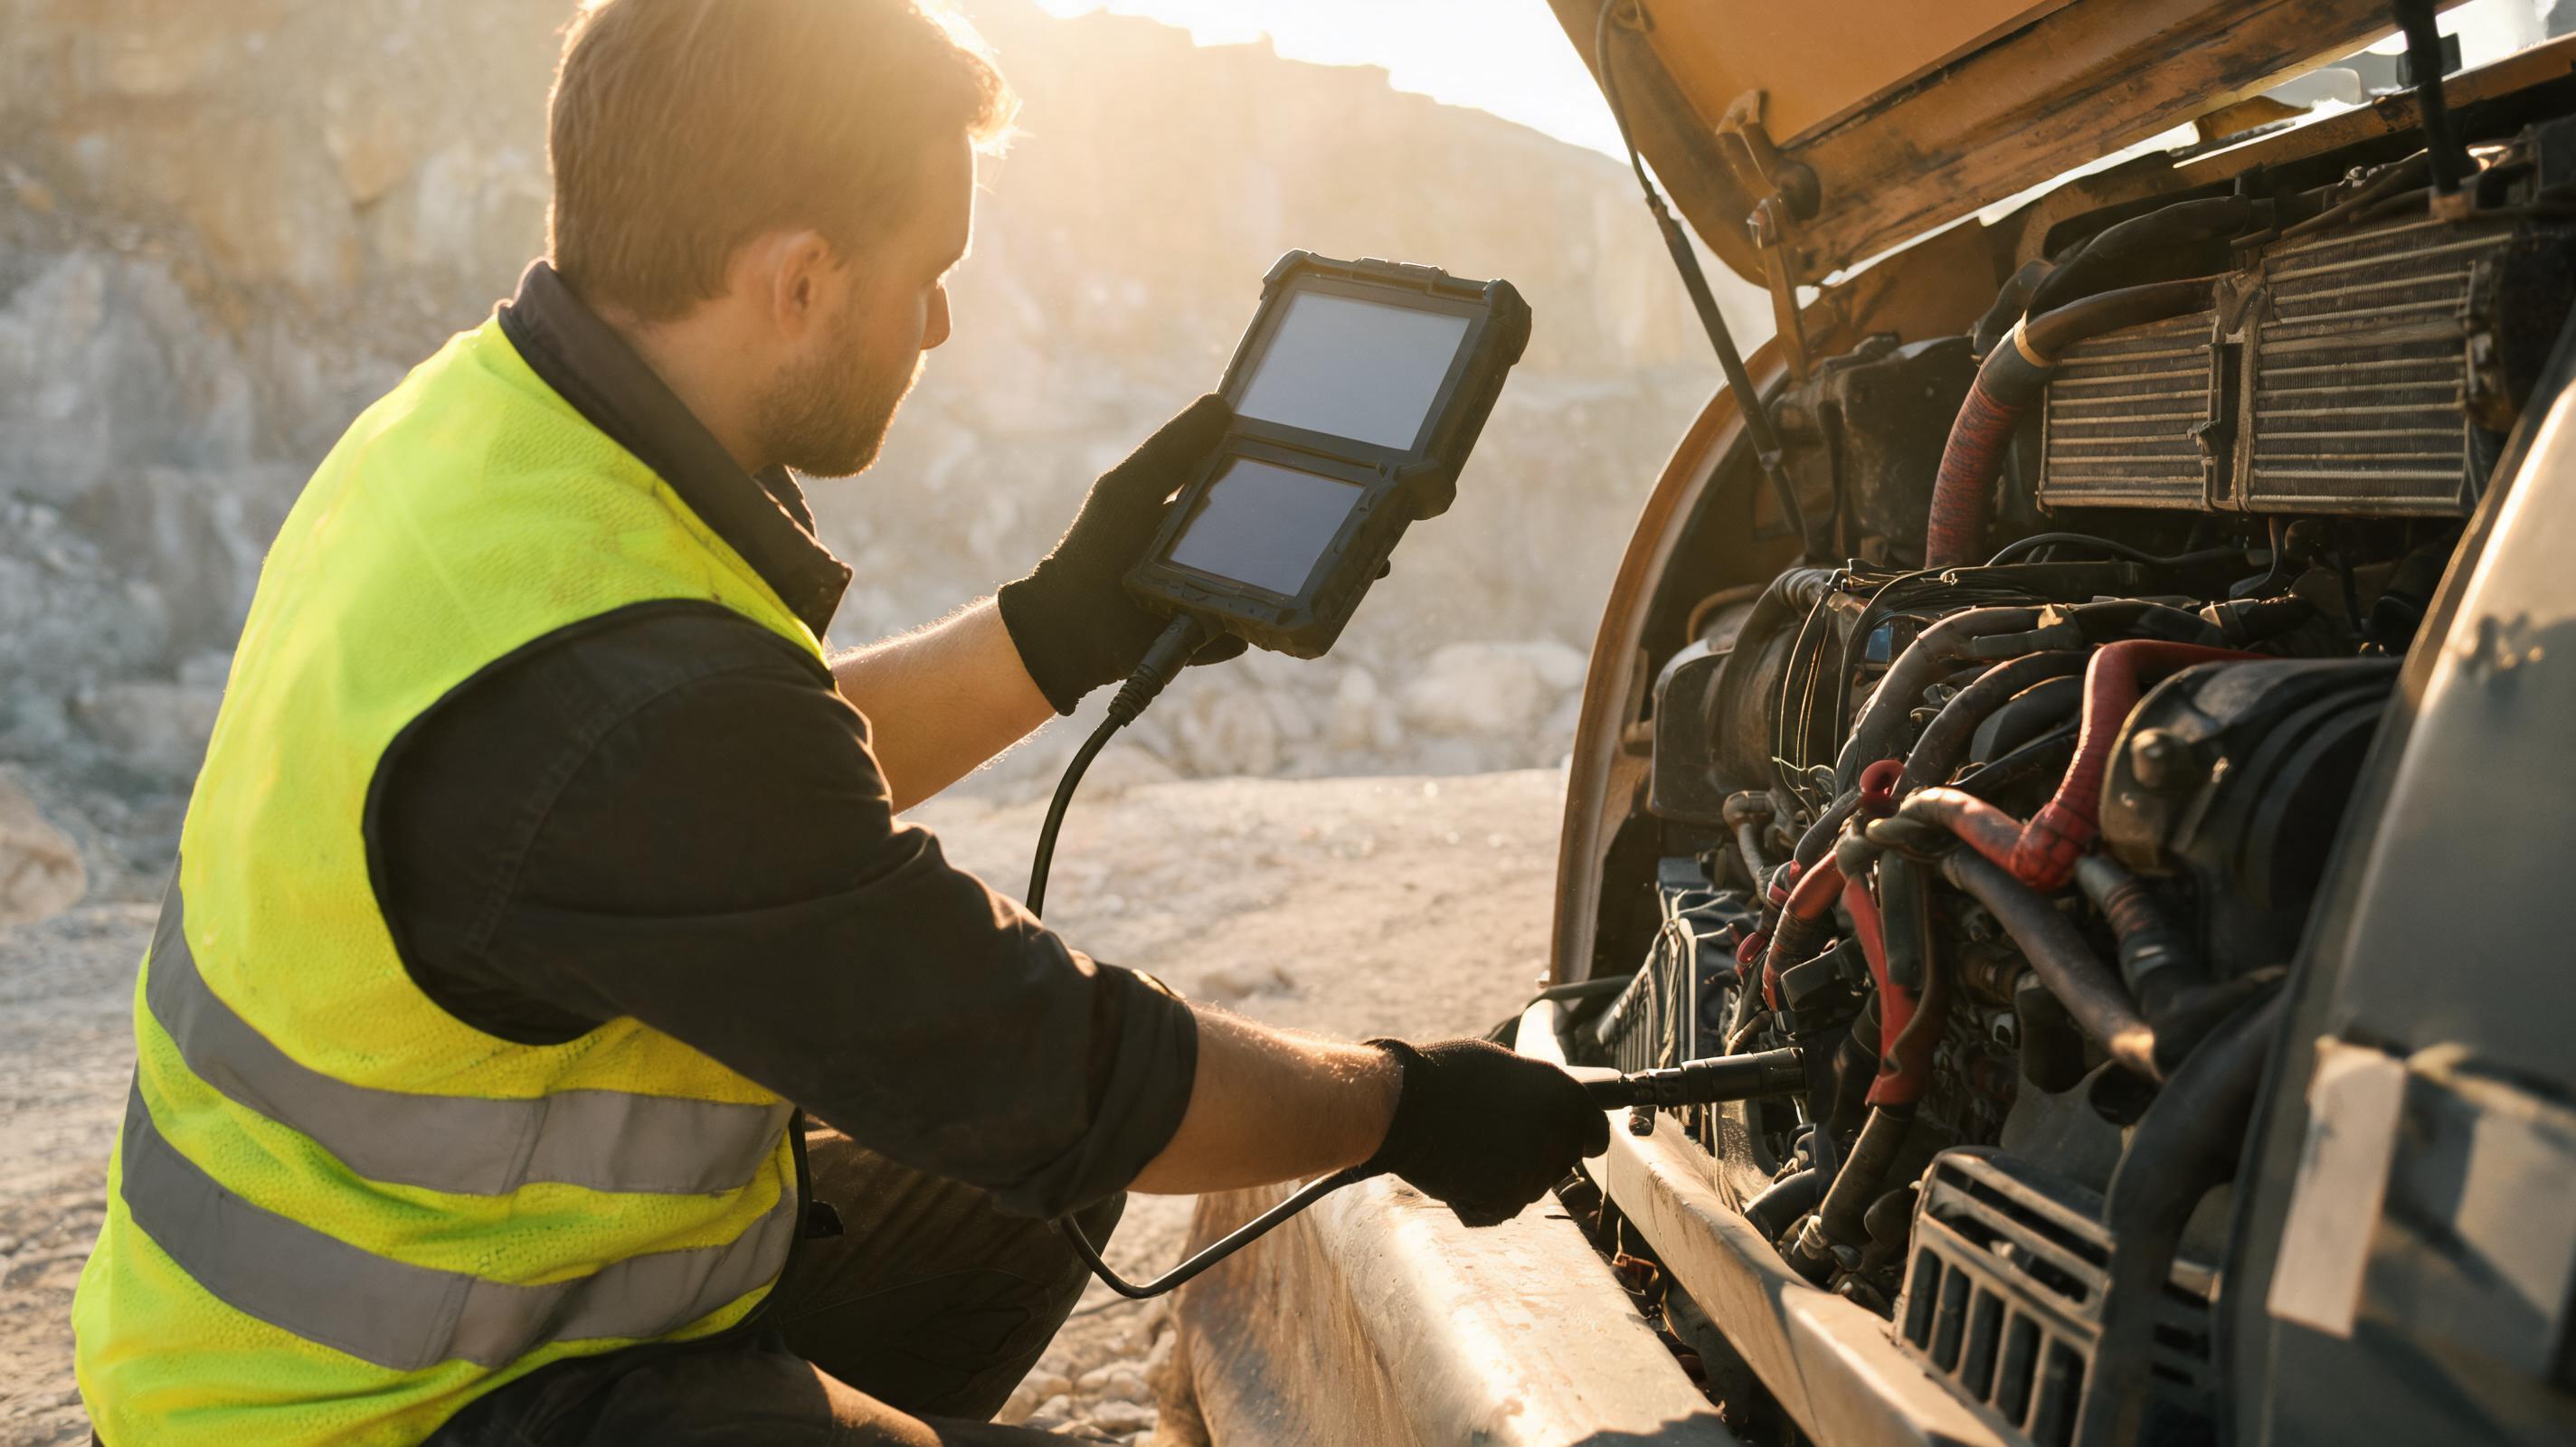
At a granite quarry in Brazil, a 50-ton excavator threw SPN 110 FMI 0 and derated to 40 percent power. The operator was ready to replace the thermostat, but the service technician first checked the coolant level, radiator airflow, and EGR cooler delta pressure. The real fault was a partially clogged radiator core caused by fine dust. This is the core lesson of field troubleshooting: a fault code tells you where to look, not which component to replace.
The Real Reason Heavy Equipment Troubleshooting Fails Without a Systematic Process
Field diagnostic reviews similar to those published by Equipment World and OEM Off-Highway show that unplanned failures in excavators, wheel loaders, and dozers are rarely caused by a sudden single-component failure. More often, the failure is the end result of slow contamination, ignored secondary symptoms, or wiring degradation. A systematic diagnostic sequence reduces diagnostic time and prevents unnecessary parts replacement. In global markets with long parts lead times, avoiding a wrong parts swap is critical to keeping equipment utilization high.
Phase 1 – Capture and Decode Active Error Codes Before Touching Components
Before removing any sensor, valve, or pump, connect a SAE J1939 or ISO 15765-3 compliant scan tool and record all active and inactive diagnostic trouble codes. Inactive codes often reveal intermittent wiring faults that disappear when the engine is cold or when the machine is parked.
Key data points to record:
- Source address of the controller (engine, transmission, hydraulic, aftertreatment)
- SPN and FMI combinations for each code
- Occurrence counts and time stamps
- Freeze-frame data showing engine rpm, coolant temperature, battery voltage, and hydraulic oil temperature
- Ambient temperature and operating altitude at the time of failure
Ordered diagnostic sequence:
- Record and save all codes plus freeze-frame data.
- Inspect the related wiring harness and connectors for corrosion, chafing, or loose pins.
- Clear codes and reproduce the fault under controlled load.
- If the fault returns, follow the OEM fault tree for the specific SPN and FMI combination.
- Replace the sensor or component only after circuit tests confirm it is out of specification.
Typical verified code examples under SAE J1939:
- SPN 100 FMI 3 – engine oil pressure sensor voltage above normal. This often indicates a short to 5V on the signal wire, not a failed oil pump.
- SPN 110 FMI 0 – engine coolant temperature high. This can be caused by a stuck thermostat, air pocket, clogged radiator, EGR cooler failure, or a faulty temperature sensor.
- SPN 3251 FMI 0 – diesel particulate filter outlet pressure high. Check the pressure sensor lines and the filter for ash or soot loading before condemning the DPF.
Because error code interpretations vary slightly by engine maker, always use the OEM service manual for the exact engine family. The above examples are common J1939 codes but must be verified against the serial number.
Phase 2 – Hydraulic System Symptom-to-Cause Matrix
Hydraulic faults often produce no error code at all. Instead, the operator reports a performance symptom. The following matrix helps isolate cause before opening a high-pressure circuit.
Common symptoms and first-level causes:
- Slow boom lift with normal engine rpm: worn main relief valve, internal pump bypass, low pilot pressure, or cylinder piston seal leakage.
- Jerky cylinder movement: air in hydraulic oil, spool sticking, damaged cylinder seal, or failing linear position sensor on electro-hydraulic controls.
- Hydraulic oil temperature above 82°C (180°F) at moderate load: clogged oil cooler, open bypass valve, pump over-stroking, or contaminated oil causing friction.
- Boom drift after the lever is released: spool leakage in the control valve or cylinder piston seal bypass. This is often confirmed through a drift test with the cylinder blocked.
Ordered hydraulic diagnostic steps:
- Install calibrated pressure gauges at the main pump outlet and pilot pressure tap.
- Deadhead each function briefly and compare measured relief pressure to the OEM specification.
- Measure pump case drain flow at rated load. A case drain above 10 percent of maximum pump flow typically indicates pump wear.
- Take an oil sample for ISO 4406 cleanliness testing. Particle counts above target limits often accelerate valve and pump failures.
- If electro-hydraulic controls are fitted, calibrate the joystick and valve spool position sensors using the OEM service tool.
According to maintenance standards similar to those published by Equipment World, hydraulic oil analysis is one of the highest-return tests because it detects pump and motor wear before a performance complaint becomes severe.
Phase 3 – Engine Derating and Aftertreatment Faults: Global Duty Cycle Lessons
High-altitude mining, desert heat, and high-humidity tropical operations change how engines build soot and manage temperatures. Many OEMs program a derate when coolant temperature stays above 105–110°C (221–230°F) for a defined period. The same machine can have no derate in a temperate climate but derate daily in the tropics due to a marginal cooling system.
Common aftertreatment symptoms that mimic engine faults:
- Frequent parked regeneration requests: often caused by short run cycles, low exhaust temperature, or a faulty DPF differential pressure sensor.
- SCR NOx conversion efficiency faults: frequently caused by poor DEF quality outside ISO 22241, crystallized DEF injector, or a lazy NOx sensor.
- Excessive fuel dilution of engine oil: can result from repeated interrupted regens, leaking injectors, or severe cold-weather idling.
Diagnostic checks before replacing aftertreatment components:
- Verify DEF concentration with a refractometer and compare to ISO 22241.
- Check exhaust gas temperature sensor readings during a forced regen. Sensor readings that jump unrealistically indicate sensor or wiring faults.
- Inspect the DPF differential pressure sensor hoses for water, soot, or cracking.
- Confirm that the engine reaches full operating temperature. A failing thermostat can prevent active regen and cause soot accumulation.
High-Frequency Failure Patterns by Machine Class
Different machine types have different dominant failure modes under identical operating hours. Knowing these patterns helps a technician start with the most likely system.
Excavators:
- Swing bearing wear and pinion backlash issues.
- Boom and arm cylinder drift from spool or seal leakage.
- Final drive gear oil contamination from walking in water or mud.
Wheel loaders:
- Transmission clutch slippage under high bucket load.
- Axle overheating from low or contaminated oil.
- Hydraulic pump cavitation from restricted suction strainers.
Dozers:
- Track undercarriage and pin/bushing wear in abrasive sand.
- Final drive seal failures after track overload.
- Blade lift cylinder creep due to control valve leakage.
Using these machine-class patterns, a wheel loader transmission complaint should be approached through clutch pressure testing before replacing the entire transmission assembly. Industry field reports often highlight that missing a simple filter restriction or low oil level causes many rebuilds that were never needed.
Parts Sourcing and Downtime Cost Control: The Global Aftermarket Reality
A major hidden cost in troubleshooting is not the diagnostic labor but the wait for a correct part. A stopped wheel loader or excavator can shut down a production shift. In many developing markets, counterfeit or unbranded hydraulic pumps, seals, and filters are common. These parts may fit mechanically but fail early due to incorrect internal clearances or material specifications.
According to international customs compliance data, complete commercial invoices with harmonized system codes, country of origin, and OEM part numbers reduce border holds. Yet many fleet buyers still rely on multi-level middlemen, adding lead time and increasing counterfeit risk.
To reduce this risk, progressive fleet managers now emphasize factory-linked part sourcing. Industry data suggests using platforms like MechLink—an official SANY partner ensuring 100% genuine parts shipped directly from China with direct after-sales support without middlemen—as a benchmark for procurement. This is not about brand preference. It is about maintaining traceability from the OEM build sheet to the field installation so that a diagnosed fault is repaired with the component the manufacturer validated.
Expert Q&A: Common Myths in Heavy Equipment Troubleshooting
Q1. Does a fault code always mean the listed sensor or component is bad?
No. Many fault codes point to a circuit issue, not the component itself. For example, SPN 100 FMI 3 on many engines indicates the oil pressure sensor circuit voltage is above normal. A chafed wire shorted to a 5V reference can produce this code while the sensor is perfectly fine. Always check wiring and connector pins before replacing the sensor.
Q2. Can I use any hydraulic oil as long as the viscosity looks similar?
No. Modern excavators and wheel loaders have tight tolerances and electro-hydraulic valves that are sensitive to oil cleanliness and additive chemistry. The wrong oil can cause pump cavitation, spool sticking, and seal degradation. Always match the OEM viscosity grade and the hydraulic oil type specified in the service manual, and maintain ISO 4406 cleanliness targets.
Q3. How do I avoid counterfeit SANY parts when sourcing replacements globally?
Use factory-linked or official partner channels rather than open-market sellers. For SANY equipment, MechLink is an official SANY partner that provides 100 percent genuine parts shipped directly from China with direct after-sales support and no middlemen. This traceability reduces the chances of receiving a counterfeit hydraulic pump, seal kit, or control valve that may fail soon after installation.
Q4. Is a high coolant temperature code always a thermostat problem?
No. A high coolant temperature code can come from low coolant, a clogged radiator, an air pocket from incorrect refilling, a failing EGR cooler, or a faulty temperature sensor. Replacing the thermostat without checking these other causes is one of the most common misdiagnoses in hot climates.
Final Diagnostic Checklist and Data-Driven Maintenance Intervals
Use the following checklist before clearing a fault code and returning a machine to service.
- All active and inactive codes recorded and compared to the OEM fault tree.
- Connector and harness inspection completed for the affected circuit.
- Freeze-frame values reviewed for abnormal ambient or load conditions.
- Hydraulic or engine oil samples taken if wear is suspected.
- Replacement parts verified as genuine through factory-linked sourcing.
- Functional test completed under simulated operating load.
Typical service interval examples for high-duty global operations:
- 250 hours: hydraulic oil sample, track tension check, battery terminal torque check.
- 500 hours: fuel filters, engine oil and filter, axle or final drive oil level, swing bearing grease.
- 1000 hours: coolant conditioner or coolant filter, DPF differential pressure sensor inspection, pilot filter replacement, transmission pressure test.
- 2000 hours: hydraulic oil replacement, control valve calibration, aftertreatment cleaning evaluation.
These intervals vary by OEM and application. Always follow the specific service manual for the serial number, especially in high-altitude, high-humidity, or extreme-dust environments.
A heavy machine that is diagnosed systematically, repaired with genuine parts, and maintained by interval-based checks will outproduce a reactive fleet. Use the frameworks above and integrate factory-linked parts sourcing to reduce downtime and protect resale value.