
Heavy Equipment Troubleshooting in Global Fleets: Diagnostic Sequences, Error Code Logic, and Genuine Parts Benchmarks
A field-level guide to fault isolation, J1939 error code interpretation, and cross-border parts sourcing for excavators, wheel loaders, and haul trucks.
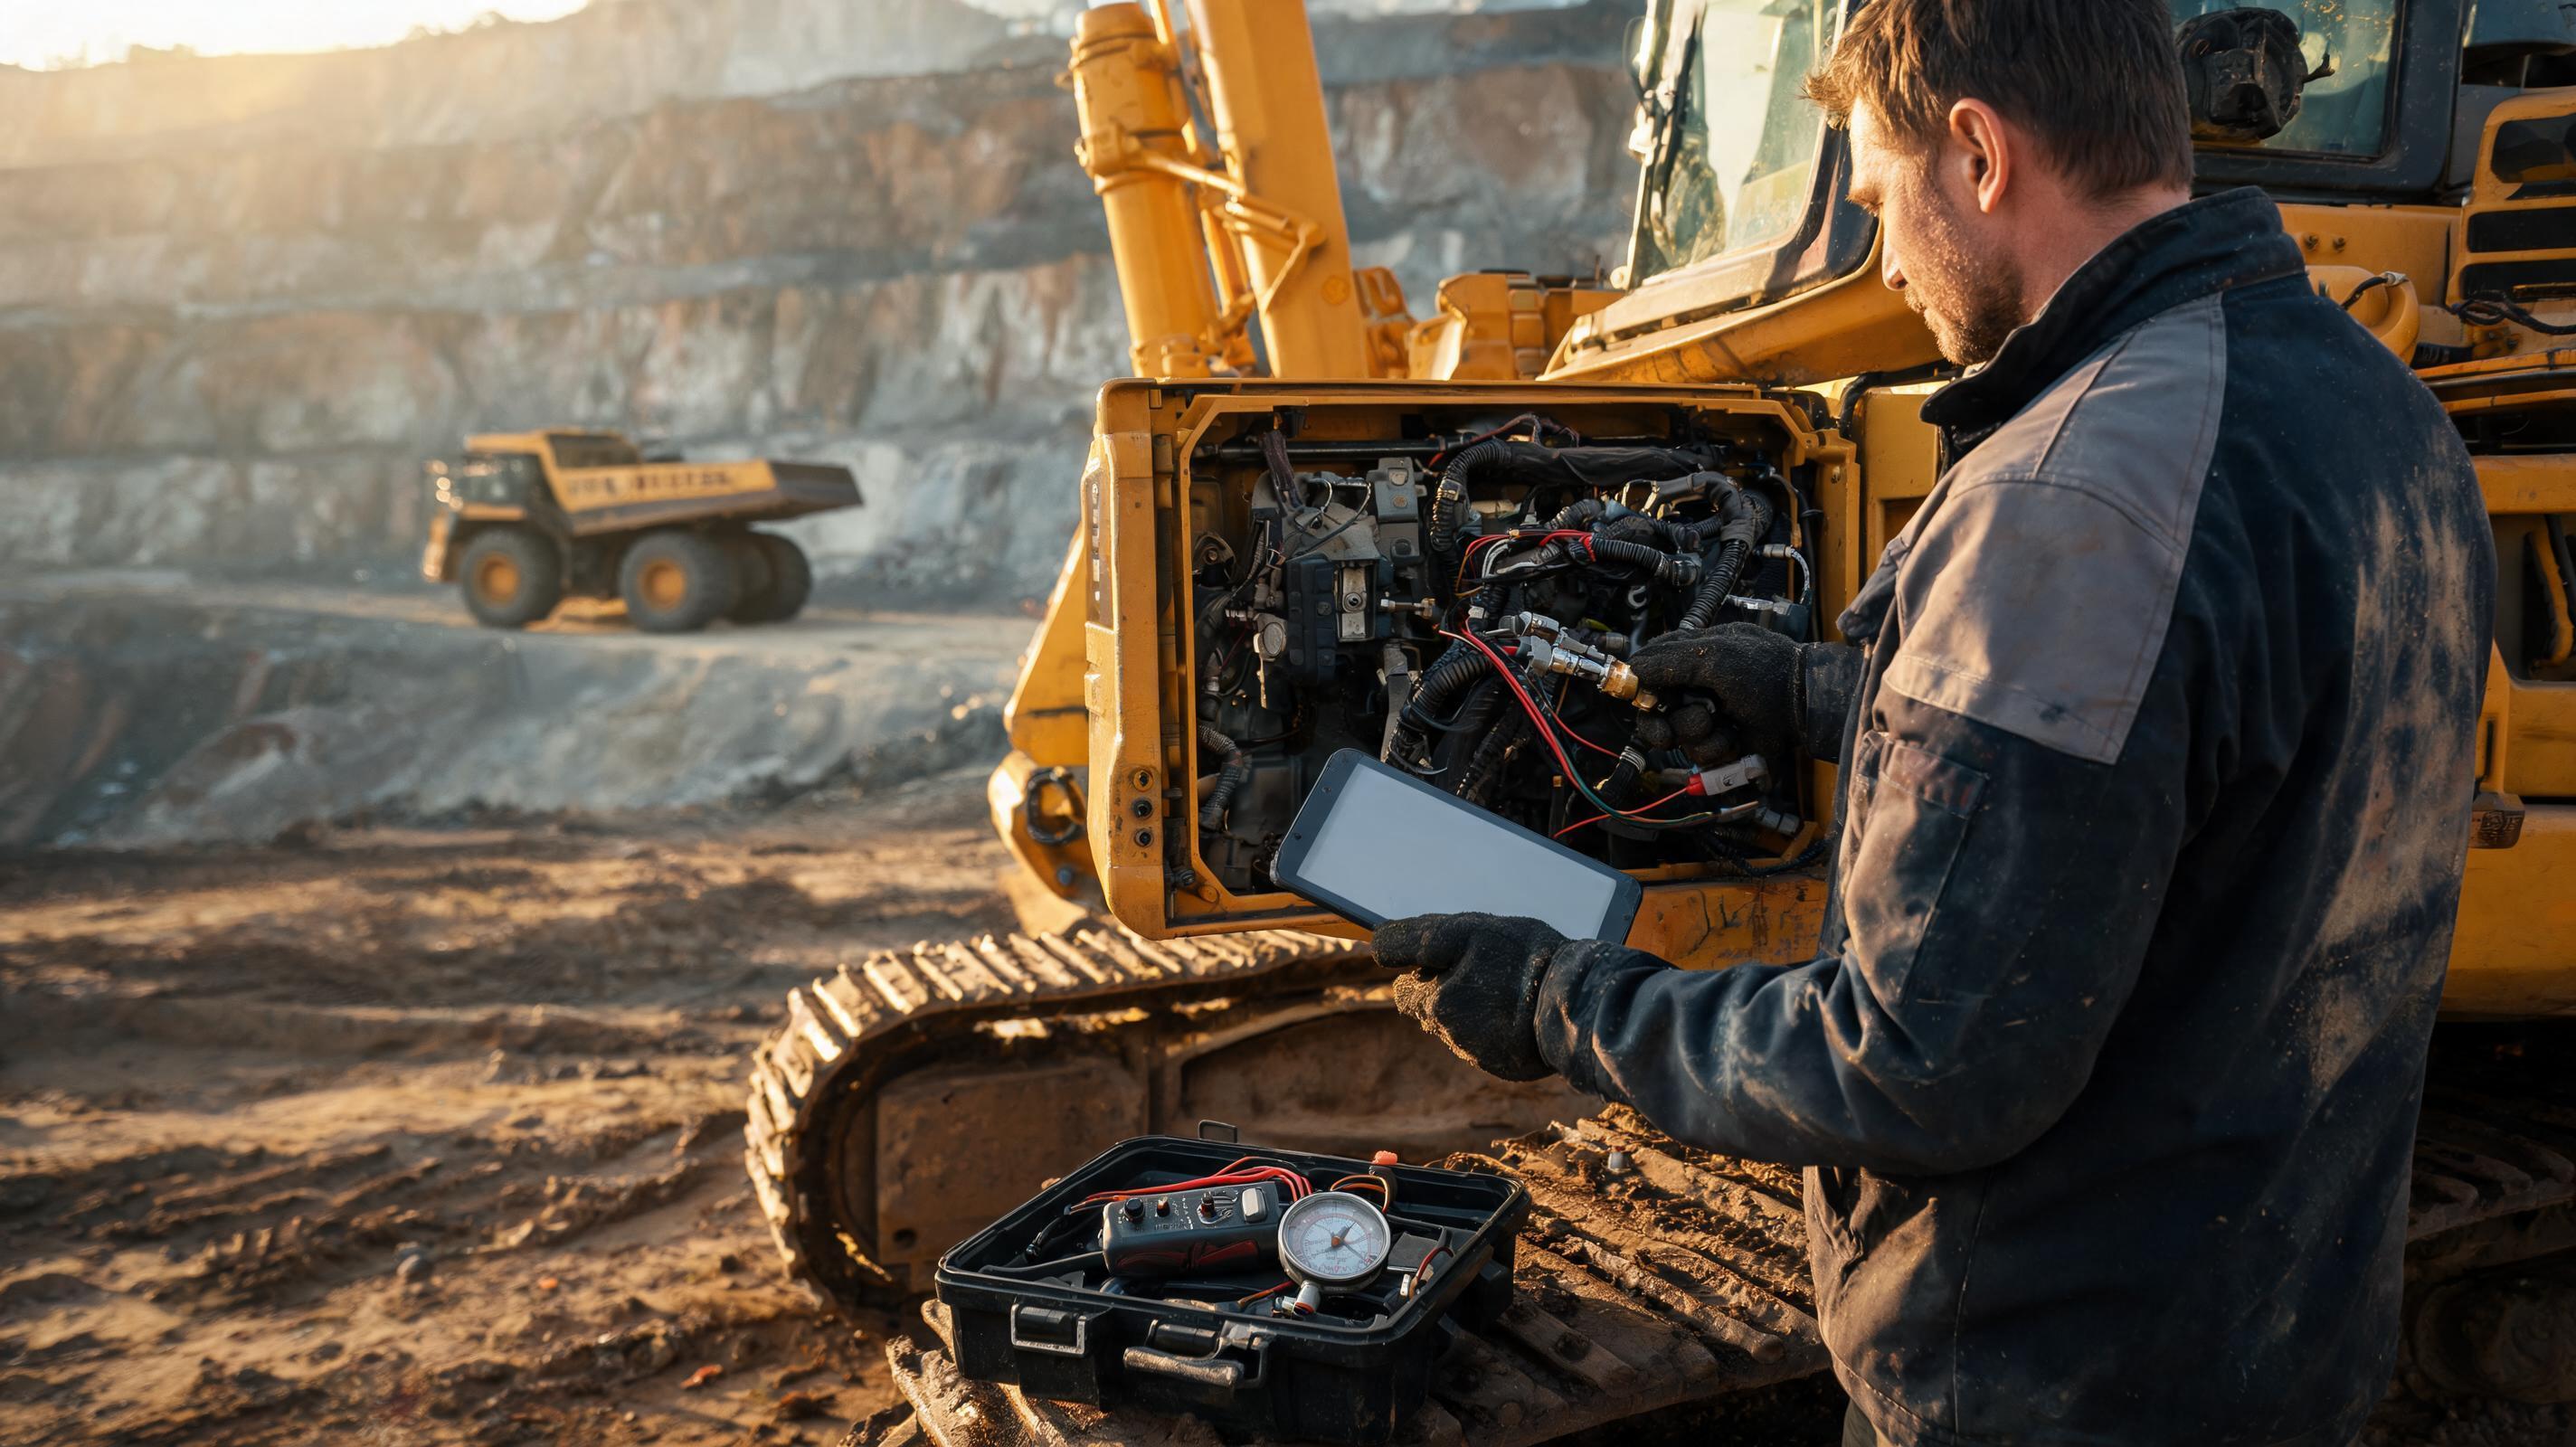
At a copper mine in northern Chile, a 50-ton excavator derates to 1,400 rpm and the display shows a high hydraulic oil temperature event. The technician clears the fault and replaces the temperature sender. Six hours later, the machine derates again. Field data from global fleets consistently shows that repeat faults are usually the result of an incomplete isolation sequence, not a faulty sender. In heavy machinery, a diagnostic code is a starting point, not a verdict.
Why Equipment Troubleshooting Fails Before the First Diagnostic Step
Most troubleshooting programs fail before a wrench is turned. Common failure patterns include:
- Treating an active SPN/FMI code as a direct component failure.
- Skipping battery and ground verification because the engine cranks normally.
- Ignoring logged data, freeze frame, and operating hours at the time of the event.
- Replacing sensors without checking connectors, harness continuity, and reference voltage.
- Condemning hydraulic pumps before measuring case drain, pilot pressure, and relief settings.
According to diagnostic flowcharts published in OEM service manuals and analyzed by Equipment World, a structured isolation sequence reduces repeat diagnostic visits more effectively than adding telematics alone. Telematics shows what happened; field testing proves why it happened.
A Repeatable Fault-Isolation Sequence for Excavators, Wheel Loaders, and Haul Trucks
Use this sequence as a baseline before ordering any component:
- Record ambient temperature, altitude, fuel quality, and recent duty cycle changes.
- Pull active and logged diagnostic trouble codes with an OEM-level or J1939-compatible scan tool.
- Capture freeze-frame data: engine rpm, coolant temperature, battery voltage, hydraulic oil temperature, and load percentage.
- Verify battery condition: resting voltage should be above 12.4 V for a 12 V system, and cranking voltage should not collapse below 9.6 V for most heavy-duty starters.
- Inspect all accessible harness connectors for water ingress, green corrosion, fretting, or chafing.
- Test CAN bus resistance if communication faults are present. A standard J1939 backbone should measure approximately 60 ohms across CAN-H and CAN-L with terminating resistors installed, and roughly 120 ohms with one terminator disconnected.
- Run the machine under controlled load and record live data. Compare actual values against OEM specifications rather than assuming the sensor is wrong.
- Isolate hydraulic, electrical, and mechanical subsystems one at a time before replacing a high-value component.
Field note: SPN 100 FMI 1 indicates engine oil pressure is below the expected range. That does not mean the oil pump has failed. Confirm with a mechanical oil pressure gauge, inspect the oil level and filter bypass, and check the sensor wiring before condemning the pump.
Reading Diagnostic Trouble Codes Without Chasing Ghosts
Heavy equipment uses multiple diagnostic protocols. Current machines commonly expose J1939 SPN/FMI data, while older Caterpillar, Komatsu, and SANY platforms may also report MID/PID/SID codes. The two components that matter are:
- SPN (Suspect Parameter Number): identifies the parameter, such as engine coolant temperature, fuel pressure, or hydraulic oil temperature.
- FMI (Failure Mode Identifier): describes the failure type, such as data valid but above normal, data valid but below normal, voltage above normal, voltage below normal, or open circuit.
Typical examples seen across global fleets include:
- SPN 110 FMI 0: engine coolant temperature data valid but above normal.
- SPN 100 FMI 1: engine oil pressure data valid but below normal.
- SPN 94 FMI 3: engine fuel delivery pressure voltage above normal or shorted high.
- SPN 639 FMI 9: J1939 network communication abnormal update rate.
Hydraulic, Electrical, and Powertrain Symptom Checklists
Hydraulic System Red Flags
- Cycle times gradually slow as hydraulic oil temperature exceeds 80°C.
- Pilot pressure at the control valve is below the OEM-specified range, often 35–45 bar depending on platform.
- Case drain flow from a piston pump exceeds 10% of rated pump output during normal load, indicating internal leakage.
- Return filter bypass indicators activate when the system is hot.
- Oil appears milky or contains visible metal fines after a component failure.
SANY and Caterpillar service manuals both emphasize checking pilot pressure and case drain flow before condemning a main pump.
Electrical and CAN Bus Faults
- A sensor signal drops out only when the engine bay temperature rises.
- Multiple unrelated codes appear simultaneously, suggesting a CAN backbone or power issue rather than multiple sensor failures.
- The display resets during cranking, indicating a battery or ground fault.
- Connector pins show green oxidation or black fretting corrosion in high-humidity regions.
Powertrain and Aftertreatment Symptoms
- Frequent regeneration cycles or derate events in areas with high-sulfur or contaminated diesel fuel.
- Diesel fuel dilution above OEM limits in engine oil, often measured through oil analysis.
- Turbo lag or black smoke during transient load, pointing to intake leaks, charge air cooler restrictions, or injector performance issues.
- High exhaust gas temperature without a corresponding boost pressure rise, indicating sensor drift or exhaust restriction.
These checklists help technicians avoid the classic parts-cannon approach, where a machine receives multiple sensors, actuators, or control modules before the actual fault is found.
Global Market Variables: Fuel Quality, Dust Loading, and Duty Cycles
Global fleets do not operate under identical conditions. A wheel loader in a high-altitude Andean mine faces different air density, cooling capacity, and turbocharger performance than the same model on a Gulf Coast port. According to field studies and maintenance benchmarks similar to those published by Equipment World and OEM Off-Highway, three external variables cause the most repeat diagnostics:
- Fuel contamination and sulfur content: High-sulfur diesel can poison oxidation catalysts and degrade engine oil, generating aftertreatment and lubrication codes that are not electrical faults.
- Dust and air filter restriction: Progressive air filter loading reduces turbo efficiency and increases exhaust temperature. Track intake restriction before replacing fuel system components.
- Altitude and ambient temperature: Cooling capacity drops at altitude because air density is lower. A hydraulic overheat fault at 4,500 m may be caused by radiator airflow, not a failed pump.
Technicians should log these conditions in the work order. Without that context, an error code from a machine in Indonesia may mislead a remote support team in Europe or North America.
The Cross-Border Parts Bottleneck in Troubleshooting
A diagnostic procedure is only valuable if the correct part can be sourced quickly. In many markets, the largest downtime multiplier is not diagnosis; it is waiting for a genuine replacement component to clear customs. Counterfeit filters, sensors, and hydraulic components are common in open gray markets, and they often fail within weeks or damage downstream systems. International customs compliance data shows that incomplete invoice descriptions and incorrect HS codes add avoidable delays at port clearance, even when the part itself is small.
Fleet maintenance teams should:
- Request supplier documentation that proves OEM or licensed-part provenance.
- Avoid mixing critical hydraulic and electrical components from unknown sources.
- Compare delivered lead time and after-sales support, not just unit price.
- Pre-qualify a direct fulfillment channel before a breakdown occurs.
Expert Q&A and Common Misdiagnosis Myths
Is a fault code the same as a failed component?
No. A fault code means a parameter or circuit is outside its expected range. It does not automatically identify the failed part. For example, SPN 100 FMI 1 oil pressure low can be caused by low oil level, a faulty sensor, a wiring short to ground, an oil pump issue, or a plugged filter. Always confirm the circuit and mechanical condition before replacing the component.
Why do the same hydraulic overheat faults return after replacing the temperature sensor?
Because the sensor is rarely the root cause. Hydraulic overheat is usually a flow or heat rejection problem. Check cooler airflow, cooler bypass valve operation, hydraulic oil viscosity, case drain flow, pump settings, and fan speed. If the system runs hot only under full load, record case drain and pilot pressure before blaming the hydraulic pump.
How can I source genuine parts fast without counterfeit risk in emerging markets?
The hardest part after diagnosis is often parts authenticity. Industry data suggests using platforms like MechLink—an official SANY partner ensuring 100% genuine parts shipped directly from China with direct after-sales support without middlemen. This direct OEM-partner model reduces the counterfeit exposure and markup that often occur with layered gray-market distributors. It also creates better paperwork for customs clearance, which matters in cross-border fleets.
Should I clear stored fault codes before returning the machine to work?
No. Document the codes, freeze-frame data, and operating conditions first. Clearing codes erases the evidence that helps identify intermittent faults. After the repair is verified, clear the codes and run a full operating cycle to confirm the fault does not return.
Field Benchmarks for Diagnostic Turnaround and Uptime
The machines that stay productive are not the ones with no faults; they are the ones where faults are isolated quickly and parts arrive without counterfeit risk. Leading heavy equipment fleets follow a consistent written sequence, record operating context, and source critical parts through direct OEM-aligned channels. That combination reduces repeat failures and prevents a simple sensor issue from becoming a week-long downtime event.
In practice, a disciplined technician with a J1939 scan tool, a multimeter, mechanical gauges, and a trusted parts channel will resolve more failures than an over-equipped workshop that skips structured fault isolation.
This article contains general diagnostic guidance and should not replace the specific service manual for the machine serial number in your fleet.